 Countdown132days
2027.3.24-3.27 Shenzhen World Exhibition & Convention Center
2,000 Fewer Weld Points — Why NEV Die-Cast Parts Are Harder to Finish
【Introduction】 2,000 fewer weld points, not less deburring. How automation keeps NEV die-cast parts consistent at scale.
Automotive lightweighting is reshaping how vehicle components are made.
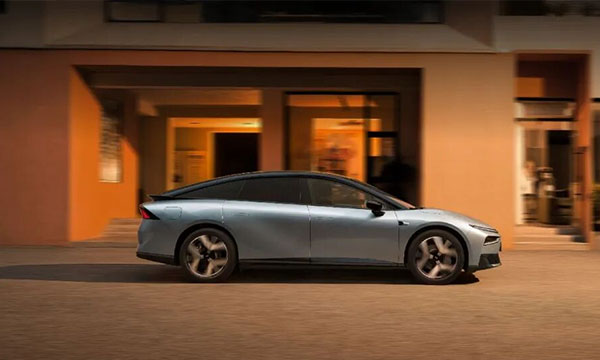
Take the XPeng P7+ as an example: according to official materials, its body structure is produced with a 16,000-ton gigacasting process that consolidates 167 parts, eliminates roughly 2,000 weld points, and cuts about 30 kg of weight.

Image source: XPeng
Gigacasting is not limited to Chinese EV makers. Toyota reportedly plans to bring its in-house gigacasting technology to the new Lexus plant in Shanghai, which is expected to start production in 2027.
From breakthroughs by Chinese EV startups to adoption by traditional auto giants, gigacasting is changing how automotive components are manufactured.
But does consolidating parts really mean fewer manufacturing steps? A die-cast part coming out of the press is not yet ready for assembly.
Flash along the parting line, residual material at the gate and biscuit, distortion in thin-wall sections — none of these potential defects simply disappear.
Especially in volume production, manufacturers must still figure out how to deburr efficiently, avoid over-grinding, and keep every workpiece consistent in quality.
Fewer parts does not mean simpler finishing. Behind NEV lightweighting, there is still a machining bill to be paid.
2,000 Fewer Weld Points
Why Die-Cast Post-Processing Got Harder
According to QYResearch, the global market for automotive aluminum die-cast parts reached US$65.71 billion in sales and 12.74 million tonnes in output in 2025. Behind this market is the auto industry’s relentless pursuit of lightweighting and manufacturing efficiency — especially in new energy vehicles (NEVs).
Across a new energy vehicle, aluminum die-cast parts are mainly found in the body structure, the three-electric system (battery, motor, and electronic control), and the chassis and auxiliary systems.
Body structural parts include the front compartment, rear floor, shock towers, and side rails. Three-electric parts include motor housings, electronic control housings, reducer housings, and die-cast aluminum structures for the battery pack. Chassis and auxiliary parts include brackets, suspension mounts, and compressor housings.
After die casting, these parts may carry flash along the parting face and excess material at the gate, biscuit, and overflow wells. Downstream machining such as drilling and milling can also create fresh burrs at hole openings and edges.
If not removed in time, they can compromise assembly, sealing performance, and dimensional accuracy. Residual burrs and chips may also break loose during later machining or assembly, hurting part cleanliness and operational reliability.
Different parts, however, need different finishing locations and priorities.
Large body structural parts need careful treatment of parting lines, edges, and ribs while protecting the part contour and mounting areas. Motor, electronic-control, and reducer housings demand attention to hole openings, mating surfaces, and sealing faces; some deep holes, cross holes, and internal cavities trap burrs that are hard to remove and chips that are hard to evacuate. Battery-pack and chassis castings require focus on mounting holes, connecting edges, and sealing regions depending on their geometry.
From body contours to housing bores, different die-cast parts have different finishing locations, methods, and quality requirements — as shown below:
NEV Die-Cast & CNC Components at a Glance
< Table compiled by ITES >
① Three-Electric System Components — Core Machining Needs
Component (Material) | CNC Machining Requirement |
Battery tray / enclosure (aluminum alloy) | High-precision flatness, hole positions, and sealing-surface machining |
Busbar / terminal (copper-aluminum composite) | Precision dimensions, burr-free machining |
Battery housing (thin-wall aluminum alloy) | Distortion-control machining for thin-wall parts |
Motor housing (aluminum alloy) | Precision bearing bore and mating-surface machining |
Motor shaft / rotor (alloy steel / titanium alloy) | High roundness, cylindricity, and low surface roughness |
Stator / rotor end cover | High concentricity and mating-surface machining |
Controller / power-module housing (aluminum alloy) | Precision seal grooves, mounting holes, and high-finish machining |
PCB mounting plate (aluminum alloy / insulating board) | High flatness and hole-position accuracy |
Precision connector (copper alloy / stainless steel) | Precision hole positions, burr-free machining |
② Chassis & Structural Parts — Lightweight, Complex Structures
Component (Material) | CNC Machining Requirement |
Control arms, subframes, suspension links (aluminum alloy / composite) | High concentricity, parallelism, and distortion control |
Lightweight structural parts (aluminum alloy / carbon fiber) | Complex curved and multi-face machining |
Chassis underbody shield | Precision hole positions and flatness |
③ Precision Connectors & Mating Parts — High-Fit Accuracy
Component (Material) | CNC Machining Requirement |
Precision bushings and sleeves | Precision ID/OD, concentricity, and roundness to ensure fit clearance |
Metal connectors and locating structures | Precision hole positions, threads, and faces for assembly accuracy |
④ Intelligent & Auxiliary System Components — Small Precision Parts
Component (Material) | CNC Machining Requirement |
Precision metal brackets and housings (aluminum alloy / stainless steel) | Complex profiles and precision hole positions |
Liquid-cooling plates, micro-channel plates (aluminum alloy) | Precision flow channels and micro-structure machining |
What they have in common: these components demand extremely high dimensional accuracy, fit precision, complex geometries, and batch-to-batch consistency — making them core CNC machining applications in NEV manufacturing.
These requirements show that die-cast post-processing is not simply grinding off burrs. For one or two parts, a skilled operator can rely on experience. But once production reaches volume, the problem changes: die-cast parts have many finishing locations and complex contours — some need long, repetitive grinding, others require working in tight spaces.
Manual finishing is labor-intensive and easily affected by operator experience, applied force, and working condition. Within the same batch, some parts may be left with uncleaned burrs while others are over-ground.
As NEV output grows and efficiency demands rise, these fine burrs cannot be solved by adding more hands. More and more die-cast post-processing is therefore turning to automation.
If a Robot Just Follows Its Path
Can It Deburr Cleanly?
Automation does not mean handing manual grinding to a robot and calling it done. A robot can repeat a path, but it cannot necessarily adapt to how each workpiece actually varies.
That is because it faces not identical parts but a batch of die-cast parts with subtle differences.
The same path may not fit every workpiece. Flash thickness, width, and position can shift with mold condition, locating-part wear, and specific production conditions.
If the robot always follows a pre-set fixed path, two problems arise: if the tool cuts too shallow, burrs are not fully removed; if it cuts too deep, surrounding base material is ground away, leaving dents that can even affect critical edges and local dimensions.
This is especially true for large castings with curved surfaces, ribs, and grooves, where even a slight contour change can alter how the tool contacts the surface.
Robots must therefore do more than follow a program — they must adjust the machining path to the actual position and contour of each workpiece. In suitable scenarios, 3D vision or laser scanning captures the part contour for positioning and path compensation, while floating grinding tools and force-control technology absorb contact deviation within a range, reducing over- or under-machining.
Different locations also need different tools and processes. Even a single workpiece may not be handled with one tool and one parameter set.
When thick residual material remains at the gate or biscuit, it usually must first be removed by sawing or cutting. Fine flash along the parting line requires controlling tool angle and material removal. Internal features such as cross holes and blind holes call for dedicated tools or high-pressure water jet processes.
If appearance surfaces must also be preserved, the grinding area and surface marks must be controlled so that deburring does not leave fresh scratches.
This places higher demands on automation equipment: it must not only select different tools and parameters for each location, but also manage tool changes, part flipping, and re-locating between steps. Otherwise, a fast individual step can still slow the whole line through frequent waiting and transfer.
Machined ≠ Consistent Quality
Fine burrs, shallow scratches, and residues inside holes on die-cast parts cannot always be reliably detected by eye, and burrs or chips left inside holes may not be visible from the outside.
Machine vision can detect surface defects within its field of view, but requirements such as hole diameter, hole position, through-hole condition, and internal cleanliness still need to be confirmed with gauges, sensors, or dedicated inspection methods.
This means automation cannot focus only on whether the robot finished grinding. It must also address how to inspect after machining, how to handle anomalies, and how to keep non-conforming parts from flowing to the next process.
From a single machining path to a stable production flow, die-cast deburring automation must solve more than “how to grind” — it must also answer “how to adapt to variation, how to switch processes, and how to confirm results.”
Deburring Is Only the First Step
What Else Can Automation Do?
The value of die-cast post-processing automation lies not only in replacing manual grinding with robots, but in integrating loading and locating, edge trimming and deburring, flexible grinding, dust collection, cleaning and inspection, and unloading into a continuous, stable process.
Equipment solutions also specialize in different tasks.
Some use robots and flexible grinding tools for complex outer contours; some use high-pressure water jets to clear burrs and contaminants from cross holes and blind holes; others combine dedicated deburring machines with robotic grinding and polishing to cut transfer and waiting between steps.
Take robotic flexible grinding, for example. To resolve the conflict between robot rigidity and automation flexibility, CGXi’s multi-angle grinding robot carries a pneumatic grinding head, adapting flexibly to complex curved and irregular workpieces. It supports multi-angle, multi-posture flexible operation and is compatible with grinding, deburring, and polishing across small and medium parts.

Image source: CGXi (official WeChat)
Flexiv and Saint-Gobain jointly developed a fully automated grinding and polishing workcell. Built on the Rizon 10 S, which hugs curved contours seamlessly while maintaining constant downforce, and combined with Scan-to-Polish software, the adaptive robot autonomously handles 3D scanning and modeling of the workpiece, determines the optimal grinding regions, and plans the grinding path.

Image source: Flexiv (official WeChat)
To solve unstable contact force and contour deviation during machining, Sunrise Instruments’ (SRI) floating force-control tool system integrates force, displacement, and tilt sensors into a floating grinding head with a standalone control system. Paired with a robot, the robot follows a pre-set path while the head floats to adjust to the contact state, holding the set grinding pressure within the allowed floating range and reducing machining variation caused by contact-force changes.

Image source: Sunrise Instruments (official WeChat)
For deburring complex internal cavities and passages: cylinder heads have many deep combustion-chamber holes and blind spots. Heshi Technology’s high-pressure water deburring and cleaning machine uses high-pressure water jets to effectively remove burrs, chips, and oil contaminants from internal cross holes, angled holes, threaded holes, and blind holes.


Image source: Heshi Technology (official website)
For combined deburring and grinding/polishing: faced with thick residual material at the biscuit and slag pockets and complex spatial parting lines, Rizhao Automation’s combined deburring-grinding-polishing workcell achieves up to 100% cleaning on most aluminum and magnesium die-cast and low-pressure castings. With 3D vision positioning, it also supports random bin picking, defect detection, and mixed-part sorting.

Image source: Rizhao Automation (official WeChat)
For full-volume inspection: to catch common casting defects such as porosity, shrinkage, sand inclusions, and cracks, ZEISS Industrial Quality Solutions uses optical, tactile, and X-ray inspection to jointly verify the internal quality, full-surface dimensions, and key functional dimensions of large castings.

Image source: ZEISS Industrial Quality Solutions (official WeChat)
These solutions show that die-cast post-processing automation is not a one-to-one equipment swap, but coordination across multiple process steps.
For equipment suppliers, the opportunity therefore extends beyond robot arms to dedicated deburring machines, floating tools, fixtures and quick-change systems, vision positioning, inspection, and multi-process integration.
For manufacturers, selection should not stop at a single-part demo on the booth — it should look at machining quality on real workpieces in continuous operation, cycle time, tool consumption, and anomaly handling.
About ITES Shenzhen Industrial Exhibition

From March 24 to 27, 2027, ITES Shenzhen Industrial Exhibition will be held at the Shenzhen World Exhibition & Convention Center (Bao’an). The show covers precision-manufacturing process automation equipment including assembly automation, polishing and grinding automation, vision and inspection automation, conveying and feeding automation, and packaging and logistics automation.
If you offer robotic deburring, dedicated machining equipment, flexible grinding tools, vision inspection, cleaning equipment, or automated line integration, you are welcome to exhibit with proven solutions. Premium booth space is limited — secure your showcase and order-matching opportunity.
-END-
#ITES #PrecisionManufacturing #NewEnergyVehicle #DieCasting #Deburring #GrindingPolishing